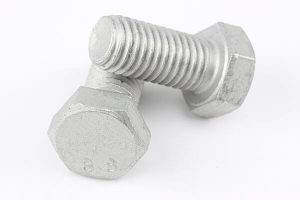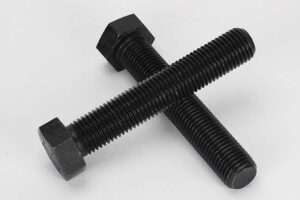
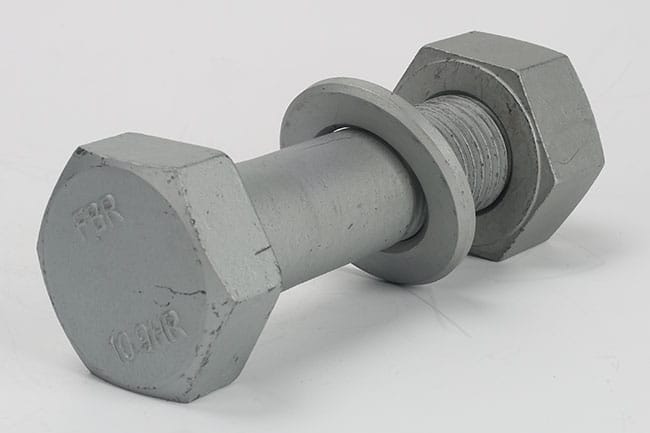
The EN 14399-4 HV bolt assembly is a matched high-strength fastening system for preloaded structural steel joints. EN 14399-4:2015 covers System HV hexagon bolt and nut assemblies with large widths across flats, metric thread sizes M12 through M36, bolt property class 10.9, and nut property class 10. It is used together with EN 14399-1 and EN 14399-2, while associated plain washers for this system are specified in EN 14399-6. Typical buyers include structural steel fabricators, bridge contractors, EPC companies, construction fastener distributors, and procurement teams working to European structural bolting requirements.
Product Overview and Key Features
System HV is designed as an assembly rather than as interchangeable individual fasteners. Its ductility concept relies mainly on deformation of the engaged threads, using a comparatively low nut and short-thread bolt. Coating, lubrication, nut fit, washers, and installation conditions therefore affect functional behavior.
- Defined HV system: class 10.9 bolts pair with class 10 nuts for preloaded structural joints.
- Metric range: eight specified sizes cover M12 through M36.
- Large hexagon geometry: increased widths across flats support structural wrenching and bearing requirements.
- Short-thread configuration: controlled thread length distinguishes the HV bolt from general-purpose fully threaded fasteners.
- Assembly-level performance: bolts, nuts, washers, coating, and lubrication form a compatible set.
EN 14399-4 HV Bolt Assembly Specifications
Specification Overview
| Item | Specification |
|---|---|
| Product form | System HV hexagon bolt and nut assembly for preloading |
| Applicable standard | EN 14399-4:2015 |
| Related requirements | EN 14399-1 and EN 14399-2 |
| Associated washers | EN 14399-6 |
| Nominal thread sizes | M12 to M36 in eight specified sizes |
| Thread form | ISO metric coarse thread |
| Bolt property class | 10.9 |
| Nut property class | 10 |
| Common finish configurations | As processed with light oil; hot-dip galvanized; other agreed coatings subject to functional suitability |
Dimensions and Thread Details
The table covers all eight nominal diameters. P is pitch, b reference thread length, s nominal width across flats, k nominal head height, and m nominal nut height. Dimensions are millimetres.
| Thread d | P (mm) | b ref. (mm) | s nom. (mm) | k nom. (mm) | m nom. (mm) |
|---|---|---|---|---|---|
| M12 | 1.75 | 23 | 22 | 8 | 10 |
| M16 | 2.00 | 28 | 27 | 10 | 13 |
| M20 | 2.50 | 33 | 32 | 13 | 16 |
| M22 | 2.50 | 34 | 36 | 14 | 18 |
| M24 | 3.00 | 39 | 41 | 15 | 20 |
| M27 | 3.00 | 41 | 46 | 17 | 22 |
| M30 | 3.50 | 44 | 50 | 19 | 24 |
| M36 | 4.00 | 52 | 60 | 23 | 29 |
For uncoated bolts, the specified external thread tolerance is 6g. Uncoated nuts use 6H. Hot-dip galvanized bolts are intended for compatible oversize-tapped 6AZ nuts. Actual bolt length must be selected from the required grip and washer arrangement; the reference thread length does not mean every diameter and length can be combined freely.
Common Materials, Grades and Surface Finishes
Material and Grade Options
The standard specifies steel components and a 10.9/10 property-class pairing rather than one universal steel chemistry. Material and heat treatment must achieve the finished properties. See Flybear’s 8.8 vs 10.9 vs 12.9 bolt strength guide for broader grade context. A generic class 10.9 bolt is not automatically an HV bolt because geometry and assembly requirements also apply.
Coating and Finish Options
Recognized configurations include as-processed steel with light oil and hot-dip galvanizing to EN ISO 10684. Other coatings can be agreed when they do not impair mechanical or functional characteristics. For class 10.9 bolts, cleaning and coating require attention to hydrogen-embrittlement risk. Confirm finish, thread accommodation, lubrication, and size combination during quotation.
Typical Applications and Selection Considerations
- Preloaded beam, column, splice, and bracing connections in structural steel buildings.
- Bridge steelwork and heavy fabricated structural connections specified for System HV.
- Industrial platforms, gantries, plant structures, and equipment-support frames.
- Infrastructure and energy structures where the project specification calls for European preloaded bolting.
See Flybear’s steel construction fastening solutions for related sourcing context. Match diameter, length, grip, washers, coating, k-class, and tightening method to the approved design. HV and HR components should not be mixed simply because the nominal metric thread matches.
Ordering and Quality Documentation
An RFQ should identify EN 14399-4, System HV, diameter, bolt length, quantity, finish, required k-class, washer configuration, and project documentation. Inspection requirements may include material verification, dimensional checks, thread gauging, hardness or tensile testing, coating inspection, and lot documentation where specified. Flybear’s quality control and inspection page describes available inspection support; the exact test scope and documents should be confirmed for each order.
Frequently Asked Questions
What sizes are covered by EN 14399-4?
The standard covers M12, M16, M20, M22, M24, M27, M30, and M36 System HV assemblies. These are metric coarse-thread sizes. Bolt length must still be selected for the actual joint grip and short-thread geometry, so the diameter range should not be interpreted as a universal length matrix.
What is the difference between HV and HR structural bolting?
HV and HR are separate European preloaded bolting systems with different geometry and ductility concepts. System HV obtains ductility mainly through deformation of the engaged threads and uses its own bolt and nut proportions. Components from the two systems should not be mixed based only on matching thread diameter.
Can an EN 14399-4 HV assembly be hot-dip galvanized?
Yes. Hot-dip galvanizing to EN ISO 10684 is a recognized configuration. The coated bolt must be paired with the appropriate oversize-tapped nut, and lubrication remains important to tightening behavior. The complete coated assembly should therefore be specified rather than ordering an independently galvanized bolt and unrelated nut.
Can other coatings be used on System HV bolts?
Other coatings may be agreed when they do not impair the mechanical properties or functional characteristics of the assembly. Buyers should specify the desired coating and project exposure conditions. Coating compatibility, thread allowance, lubrication, and the treatment process for class 10.9 steel should be reviewed together.
What information should be included in the RFQ?
Provide the standard, HV system, diameter, bolt length, quantity, surface finish, k-class requirement, washer arrangement, and required inspection documents. Include the connection drawing or bill of materials when grip, coating, installation, or project-specific requirements affect the assembly configuration.
Request a Quote for EN 14399-4 HV Bolting Assemblies
For an EN 14399-4 HV bolt assembly quotation, send Flybear Industrial the required diameter, bolt length, quantity, finish, k-class, washer configuration, and documentation needs. Include structural drawings when connection details control the selection. Submit the project through the Flybear fastener RFQ page so the requested configuration can be reviewed before quotation.